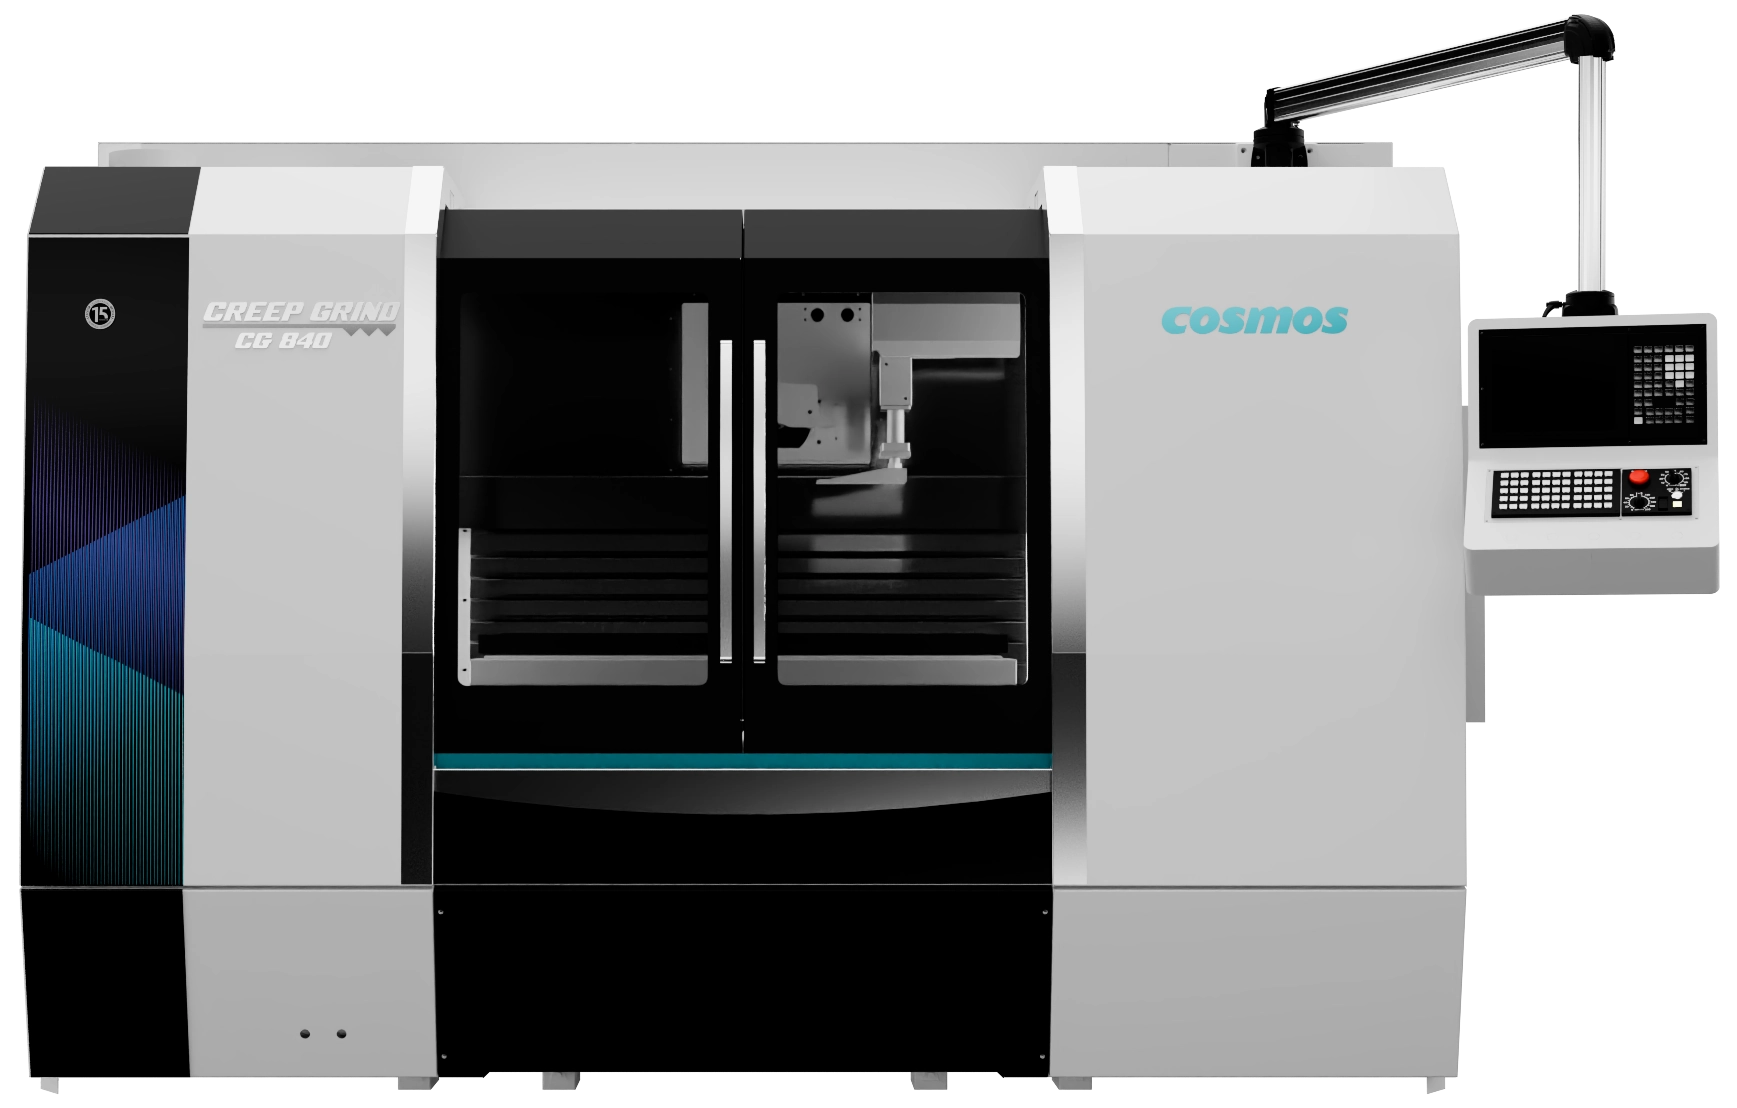
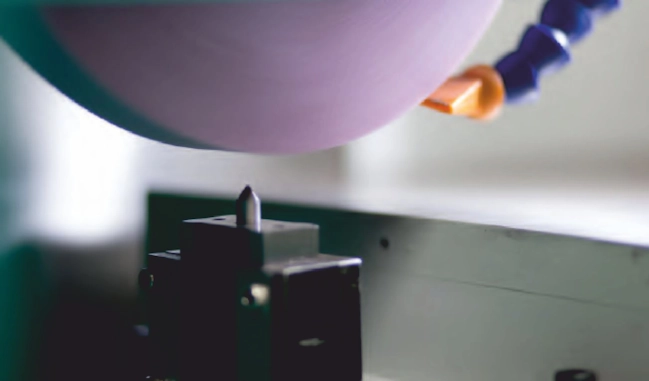
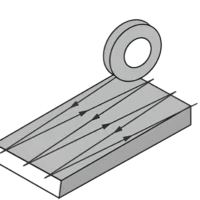
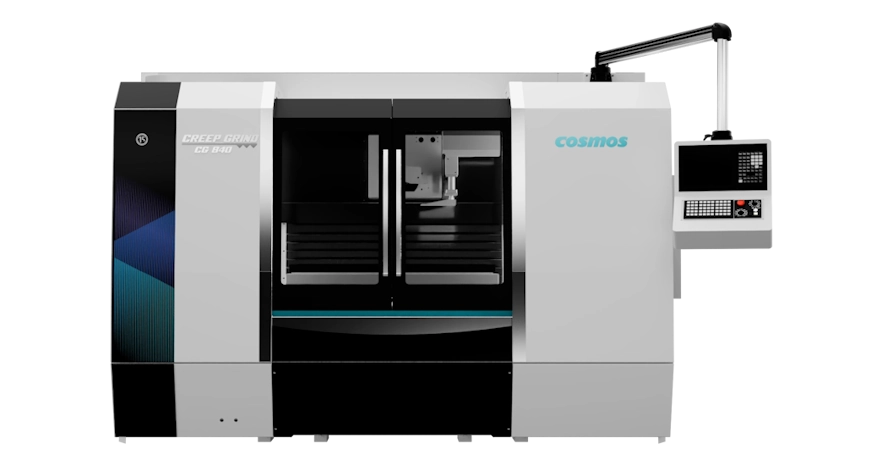
Creep Feed Grinding is a precision grinding method where the grinding wheel carves a full-depth contour into the workpiece in a single, slow pass. This process is ideal for creating intricate shapes, profiles, and features that are challenging to achieve through conventional grinding methods.
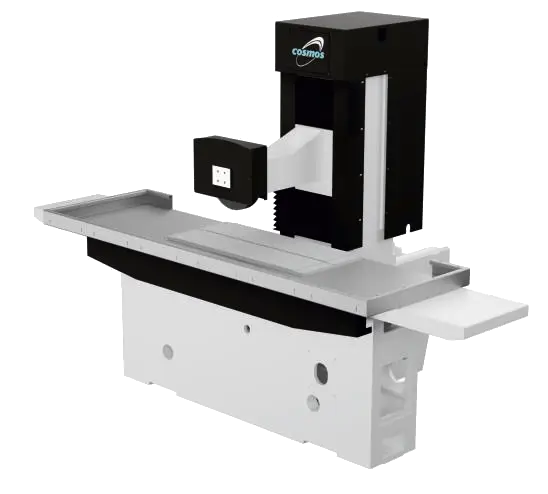
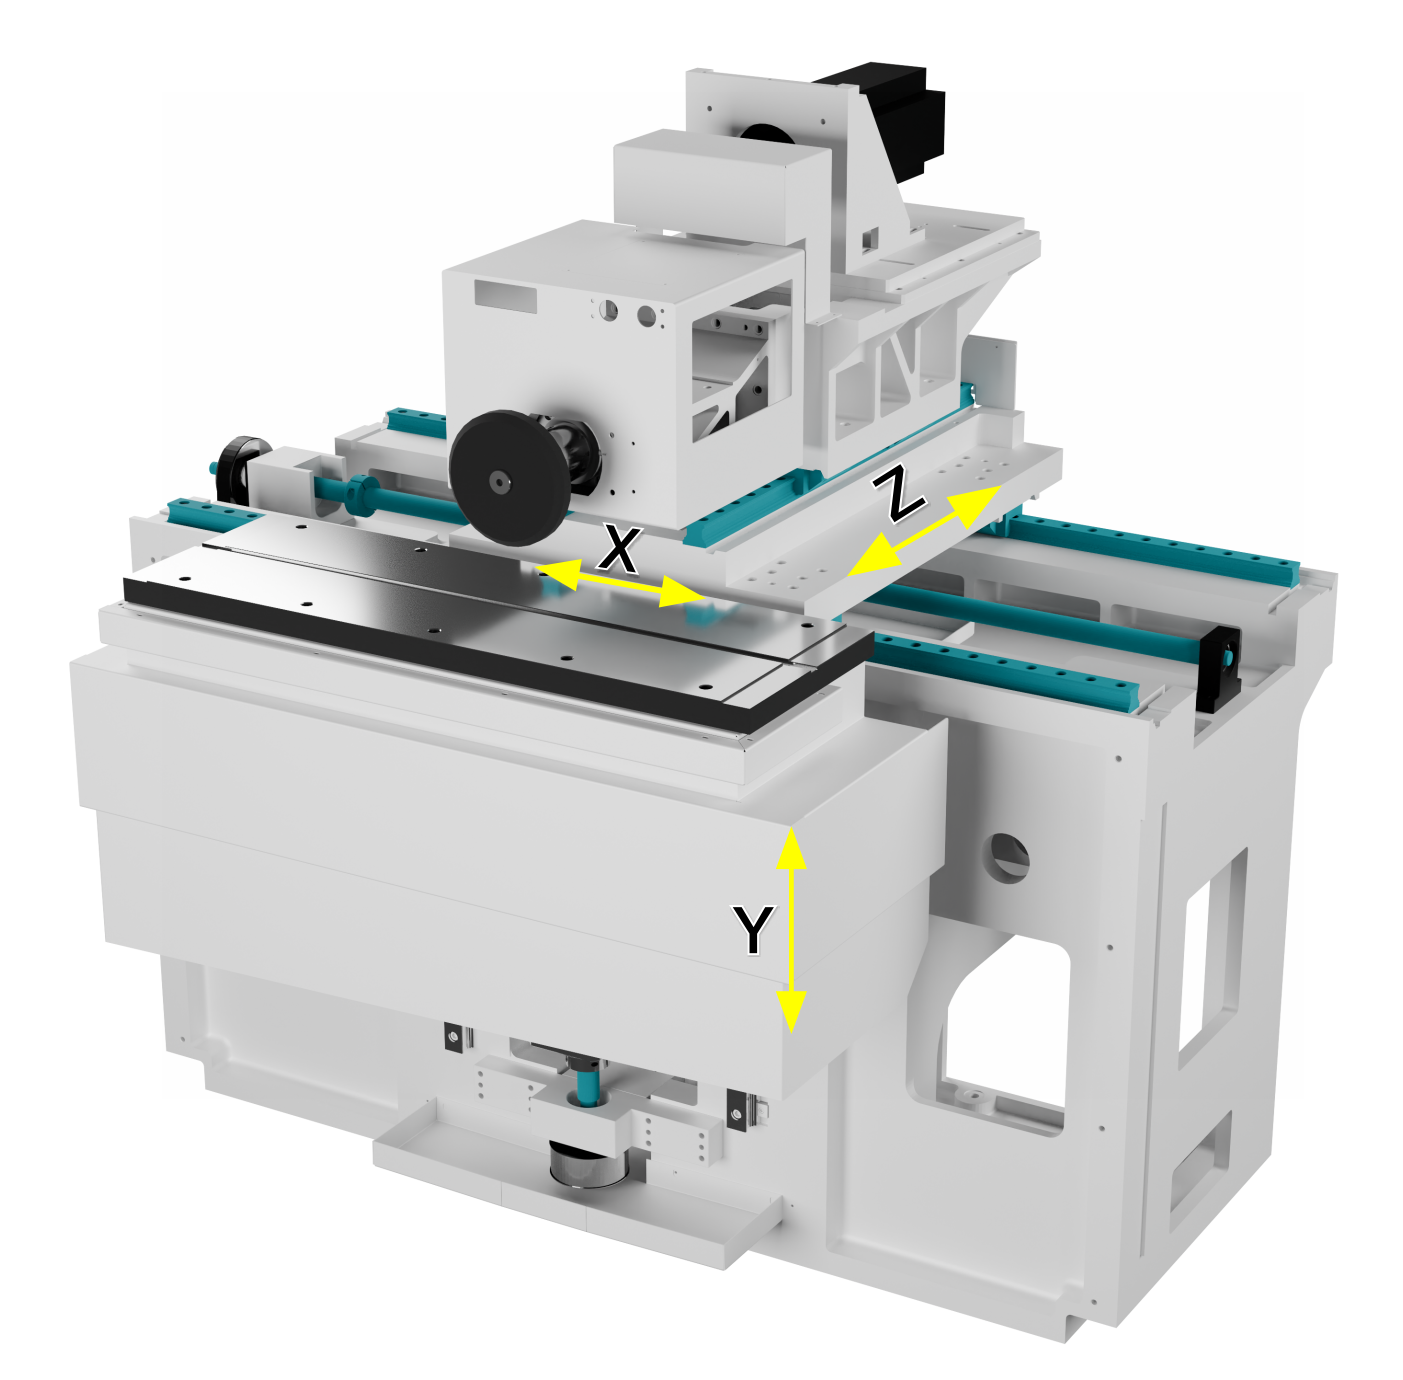
Column moving design with independent movement of all three axes. Making it long last for years and years to come. All axis move independently resulting in perfect perpendicularity in between the three axis. This ensures better flatness and parallelism.
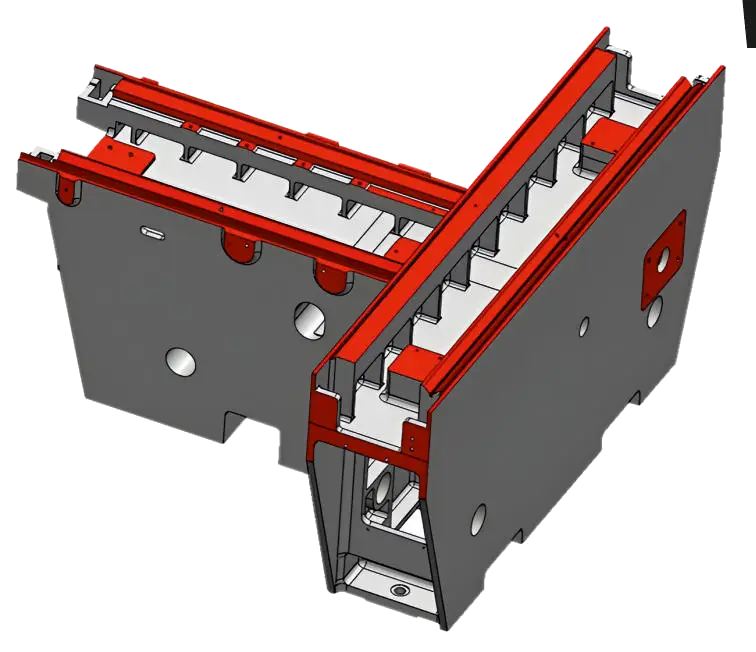
Hand scraping creates contact points and oil pockets (high and low spots) between mating surfaces, ensuring a perfect match between components. This process improves surface conformity and promotes even oil distribution for smoother motion.
Smart feature for automatic dressing on table and when the grinder enters an automatic dress cycle, the table automatically positions itself where the diamond is set to dress and compensate according to operator settings and continues grinding.
Grinding Area: 800 × 350 mm
Longitudinal Travel:Â 800 mm
Cross Travel:Â 350 mm
Vertical Travel:Â 300 mm
Max. Load on Table:Â 300 kg
Spindle Motor:Â 22 kW
Spindle Speed: 1000–3000 rpm
Grinding Wheel Size Max. (OD × Width × ID): 400 × 100 × 127 mm
Rapid Traverse X Axis:Â 10,000 mm/min
Rapid Traverse Y Axis:Â 5,000 mm/min
| Sr. No. | Machine Model | Length (l) | Travel (t) | Depth (d) | Height (h) |
|---|---|---|---|---|---|
| 1 | SG-7040 | 2755 | 3150 | 1975 | 2550 |
| 2 | SG-8040 | 3350 | 3750 | 2500 | 1950 |
| 3 | SG-1050 | 3530 | 4690 | 2475 | 2900 |
| 4 | SG-1260 | 3780 | 5100 | 2730 | 2900 |
| 5 | SG-1570 | 4825 | 6475 | 3305 | 3075 |
| 6 | SG-2070 | 6335 | 8500 | 3540 | 3100 |
| Longitudinal Hydraulic |
Vertical Servo Motor with Ball Screw |


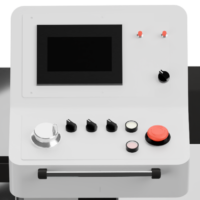
Operator skill level and fatigue reduced by eliminating manual machine operation. The complete grinding is done in auto cycle by feeding the required data in our user-friendly interface HMI. However, in case any manual operation is specifically required, it can be done by using MPG mode.
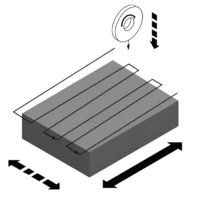
Plunge Grinding Cycle is used for slot or side face grinding operation. It can also be utilised for top face grinding when component width is lower than wheel width. Here cross axis is fixed, and only vertical axis will move downward after each table reversal.
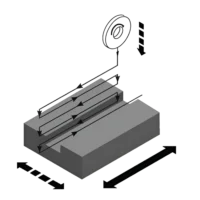
In Intermittent Traverse Cycle, the cross axis will move further after each table reversal for surface grinding operation.
In Continuous Traverse Cycle, the longitudinal and cross axis will move simultaneously.
This feature is only available with machine having servo motor in cross axis.
High-tech Products for Unmatched Performance